Six months after the brand red was signed off, the reprint packaging still doesn’t match—is the issue the retained sample or the printer?
Quotable conclusion: The standard color in VI system design usually is not a single color code that works everywhere, but a combination of a physical reference color, scene-specific target values, and tolerances. Screens, offset printing, spot colors, and inkjet printing belong to different color-rendering systems, and direct conversion does not equal consistent output. So when the screen looks right, the print looks dull, and the storefront inkjet looks orange, what should be trusted is the physical reference in the sample signed by both sides; HEX and CMYK are only approximations that move toward it. If a reprint still doesn’t match, it is often not that the wrong color code was chosen originally, but that the retained-sample record did not note the paper, process, and viewing light source.
The essence of a standard color is a set of target values plus tolerances, not a single number
Open the color page of a typical VI manual and you will see a row of color chips for the primary color and another for secondary colors, with CMYK, RGB, or HEX listed underneath, plus a spot color number. Many people assume these are different ways of writing the same color, but they are approximations under different color-rendering systems, and conversion between them naturally has deviations.
- Screen (RGB/HEX): additive color, formed by emitted light, with a wide gamut. Vivid colors such as fluorescent orange and electric blue usually cannot be reproduced on paper, so screen previews can only indicate direction.
- Offset four-color (CMYK): subtractive color, based on halftone overprinting. Deep blue, orange-red, and highly saturated green are areas that commonly cannot be matched.
- Spot color ink: pre-mixed ink, printed in one pass, with relatively better batch-to-batch stability, but still affected by paper and viewing light source.
- Inkjet, UV, and screen printing: the ink systems and substrates differ even more, and outdoor use also needs to account for sunlight fading.
The same set of values shifts in production because of four variables
Based on common 2026 delivery experience, color drift is rarely because one party is careless; it is usually because four items are not aligned: substrate, surface process, equipment and ink batch, and viewing light source. When the same CMYK values are printed on coated paper and kraft paper, a one-step visual difference is within a typical range; matte lamination darkens the overall result slightly, varnish brightens it, and foil stamping and spot UV change the direction of reflection.
- Substrate: coated paper absorbs less ink and looks more vivid; uncoated paper and natural-color paper look duller overall.
- Process layering: lamination, varnish, and embossing change surface reflectance, especially on dark colors.
- Equipment and batch: deviations can appear when an inkjet printer changes ink batch or an offset press changes machine.
- Light source environment: indoor warm light, outdoor daylight, and lightbox backlighting are three different color-viewing conditions.
A real site where storefront, packaging, and online hero images were renewed in the same batch
In 2026, we handled a chain-store renewal project: storefront inkjet, product packaging, and online hero images all had to be renewed within three months, the only reference at hand was a phone photo of an old hangtag, and the budget was tight. The approach was to first match colors face to face with the client using a physical color card, sign and number the retained samples, then give separate target values for inkjet and offset. For the storefront, an A3 solid patch proof was first made and pasted at the store for viewing. The first inkjet round still came out orange because the inkjet vendor changed ink batch midway; another round of patch comparison was needed before final approval, adding three to five days of schedule and one proofing fee. In this kind of project, proofing rounds and tolerance criteria usually need to be written into the contract; skipping this step usually costs rework on installation day.
Spot color versus four-color approximation: how to calculate the trade-off
The color page ultimately has to pass the budget test. The trade-off usually depends on three things: how many times this color appears in a year, whether it crosses suppliers, and whether end customers would notice a shift.
- Spot color approach: the single ink-mixing fee commonly falls within an experience range of several hundred to over one thousand RMB; proofing and ink-preparation lead time is often three to seven days longer than a regular approach; batch-to-batch consistency is better, suitable for frequently repeated colors such as the main color on the front of packaging or the base color of a storefront panel.
- Four-color approximation: no extra ink-mixing fee, and lead time is basically unchanged; deep blue, orange-red, and highly saturated green are areas where deviations are commonly larger, and differences are more obvious between batches and between factories.
- Compromise approach: use spot color or strict proofing for the primary color, allow four-color approximation for secondary colors with written tolerances, and concentrate budget on the one or two colors with high recognition.
- Not recommended: making every color a spot color, or giving only a string of CMYK values for every color—the former easily exceeds budget, while the latter effectively pushes color-decision responsibility to the production vendor.
How detailed should the color page be for the manual to be usable?
When accepting a VI manual, focus on whether the color section writes out the judgment conditions for the production vendor. You can check item by item as follows:
- Whether each color is marked with applicable scenarios and materials, rather than just several rows of values side by side;
- Whether it clearly states boundary notes such as screen values are for reference only and printing is subject to proof approval;
- Whether it provides handling criteria for special cases such as reversed white on dark backgrounds, single-color black, and metallic substrates;
- Whether it includes physical retained-sample numbers or proofing records that can be pulled directly when changing suppliers;
- Whether tolerances and acceptance methods are clearly written, instead of leaving only a sentence such as 'subject to the design file'.
A common counterexample is a color page with only one row of color chips and three rows of numbers, with no material notes and no tolerances. Such a page looks good in a proposal, but when it reaches storefronts and packaging, production vendors can only handle it according to their own experience, and the colors naturally drift further apart.
When is a full set worth writing, and when is it unnecessary?
The cases that need a complete color specification are fairly clear: more than five or six types of materials to be produced within a year, involvement of more than two production vendors, or brand recognition highly dependent on a specific color, such as the main color on the front of packaging or the base color of a storefront panel—in these cases, a reference color plus grouped target values is a necessary investment.
For small brands whose materials only go online and through short-run digital printing, no more than two or three types per year, and with no cross-supplier collaboration, there is no need for spot colors and multiple proofing rounds. One set of sRGB values plus one physical proof is usually enough; forcing a thick specification instead lengthens the cycle and raises costs. The judgment criterion can be simplified to one sentence: Will this color be repeatedly produced on equipment you do not control? If yes, it is worth writing a specification; if no, there is no need to add budget for it.
Common questions
If the manual only gives CMYK and HEX, with no spot color number or applicable materials, is that enough for a storefront?
Usually not. Inkjet printing is not offset printing; CMYK values must be matched again on an inkjet printer. Without a spot color reference or physical reference, adjustment can only rely on experience. It is advisable to add a set of physical references confirmed by proofing and specify the material.
If a color was confirmed six months ago and this reprint still doesn’t match, which side should be checked first?
Check the retained-sample record first: what paper, what process, and what light source were used when that sample was viewed. If the record is missing, responsibility is hard to determine; if the record is complete, then compare the printer’s batch and machine, and in most cases the specific step can be identified.
If two printers produce the same packaging batch and the colors differ, whose problem is it?
First check whether the contract and manual specify tolerances and acceptance methods. If not, responsibility is hard to determine; if they are specified and the difference still clearly exceeds them, the usual approach is visual comparison against the retained sample under the same light source, and the party exceeding tolerance reprints or makes up the quantity.
For a brand that is just starting out, can we define only the screen color set?
If you only do online and short-run digital printing, yes; one set of sRGB plus one physical proof is usually enough. Once you move to offset printing, storefronts, or packaging, it is advisable to add a physical reference; otherwise, every change of production vendor means renegotiating the color.
If you are preparing to define VI standard colors, you can start with three things: list the materials to be produced within a year and mark their substrates; ask the designer to provide a set of physical proofs and applicable-scenario notes for each color; and write tolerances and acceptance methods clearly into the contract. If materials only go online and through short-run digital printing, no more than two or three types per year, spot colors are unnecessary; one set of screen colors plus one proof is usually enough.
-
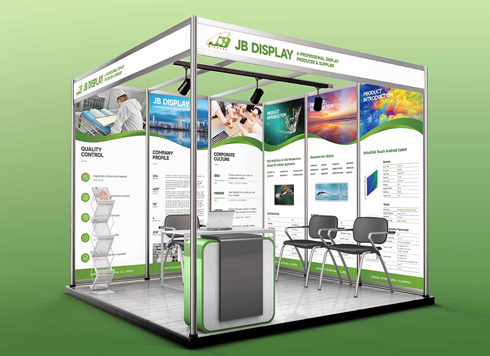 Booth Poster Design for Professional Monitor Product Suppliers
The standard exhibition booth poster projec ...
-
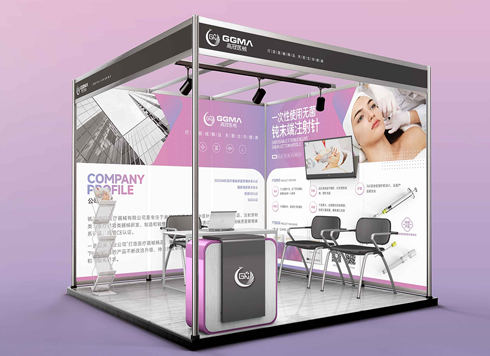 Design of Standard Exhibition Booth Posters for Beauty Instruments
Carefully designed a standard exhibition bo ...
-
 Design of Exhibition Posters for Medical Device Standards
XiYue is designing an exhibition booth post ...
-
 Collection of Brochure Design Cases in 2024 (Cover Series 02)
Our brochure design projects focus on diver ...
-
Storefront is installed and packaging is printed—will newly added supporting graphics still match the earlier materials?
Date: Nov 21, 2026 Read: 6
-
The same brand red looks different on a storefront print and a packaging box—is one color code in the manual enough?
Date: Nov 15, 2026 Read: 33
-
The sub-brand is still internal-only—should the VI system include the master–sub relationship in advance?
Date: Oct 16, 2026 Read: 46
-
Switching embroidery factories means the logo has to be redrawn—is the grid construction page the problem?
Date: Oct 10, 2026 Read: 56
-
Brand logo has only one horizontal version—when hang tags, ID badges, and packaging frames won't fit, should you add versions or force-scale?
Date: Oct 4, 2026 Read: 57