Large-area poster gradients print out in stripes — can adding noise alone fix it?
When a printed gradient shows banding — stripe after stripe — it is usually not simply a file problem, nor a problem the printer causes on its own; it is the combined result of file-side color-step span, color mode, and image precision overlapping with process-side screening method, flat-tint control, and equipment condition. The suggested order of judgment is: first check whether the file provides enough color steps, then confirm whether the output method and paper can carry that gradient, and only then suspect the equipment. In the common 2026 project delivery practice, narrowing the gradient span, adding a little noise when necessary, and requesting a proof before release can usually push banding down to a level that is not very noticeable under actual viewing conditions.
1. The nature of banding: the color steps are stretched apart, not the file being dirty
Banding, at its core, is the human eye picking up the jump between two adjacent color steps. In an 8-bit channel, each color channel has only 256 levels; the longer a gradient is stretched and the farther apart the two end colors are, the greater the distance each single color step has to cover on its own, and the boundaries naturally show. Printing then adds another layer of variables: halftone screening, ink amount, and paper absorption all magnify jumps that were only barely hidden into visible stripes.
So whether a gradient bands depends not on whether the gradient looks good, but on whether its color steps are dense enough, whether the span is small enough, and whether the output end can reproduce it. The same gradient may be perfectly fine on screen yet show immediately on a large offset-printed surface; this difference is physical, not a matter of someone being careless.
- On the file side, look at: whether the color-step density is sufficient, whether the two end colors differ too much, and whether there is leftover transparency or compression.
- On the process side, look at: screen ruling, total ink coverage, flat-tint area, and paper and equipment stability.
2. Order of judgment: file first, then process, equipment last
This order is used because the three differ greatly in cost to change: fixing the file is fastest and cheapest; the process can be verified through proofs; equipment condition is harder to control and should not be suspected first before the previous two are ruled out. Get the order wrong, and the common outcome is the designer and the printer pointing at each other back and forth — several rounds of revisions and one reprint later, the problem is still exactly where it was.
- Step 1 — File self-check: zoom the gradient area to over 100% and look for obvious stair-stepping; confirm whether it is an extreme span such as pure white to pure black; check whether transparency, shadows, or blend modes are stacked on the gradient. This step focuses on whether the file itself has usable color steps.
- Step 2 — Output condition check: confirm whether the color mode and total ink coverage follow the specs given by the printer, whether the black in the gradient switches recipe midway, and whether the screen ruling matches the paper. This step focuses on whether the output end can reproduce that gradient.
- Step 3 — Proofing and process verification: first request a digital proof or a press proof and observe the pattern of the banding — is it fixed in the same position across the whole run, or intermittent? This step focuses on fluctuations in equipment and ink/water state.
Skip any one of the three steps and the judgment lacks a basis. Guessing where the banding comes from based only on how it looks on screen is one of the more costly approaches in this kind of rework.
3. Common file-side pitfalls
- Span too large. Gradients that run straight from deep blue to light yellow, or from pure black to pure white, tend to break more easily. By experience, the greater the lightness span and the shorter the gradient distance, the higher the chance of visible banding; narrowing the span or splitting the gradient into two transition segments is often more effective than repeatedly adding filters.
- Building a gradient from transparency, masks, or shadows. It may look soft in the software, but at output it is easily rasterized into multi-level jumps. For objects that can be changed to a solid-color gradient, try not to substitute a transparency gradient.
- The gradient sits on a low-resolution or twice-compressed image. The image itself already carries color-step breaks; output simply magnifies them. Checking image resolution against the output size before delivery is a step more easily overlooked than adjusting the gradient itself.
- Switching the recipe midway when a color gradient goes to black. If one end is a black built from four-color overprint and the other is single-color black, the mid-transition will show dirty edges or jumps. For black within a gradient, it is recommended to use single-color black, or to unify throughout according to the four-color black ratio provided by the printer.
4. Process-side variables and a set of checkable comparisons
First, an experience from the delivery floor: a common scenario in projects is that the budget only covers one proofing round, the client asks for a full-bleed gradient background on the cover, and the designer lays the gradient across the entire layout — without doing any file-side self-check before release or confirming the screen ruling and total ink limit with the printer. As a result, the first print run of over a thousand covers shows obvious stripes from top to bottom, and the plates have to be redone for another run, at the cost of not only the printing fee but also schedule delays. In this kind of rework, the problem was usually planted back at the file stage. By experience range, one press proof commonly costs somewhere in the range of a few hundred to over a thousand RMB, while a reprint often costs several times the proofing fee — an account that should be settled before work begins.
There are several process-side variables that need to be clearly communicated with the printer in advance at delivery:
- Screen ruling: the higher the ruling, the finer the dots and the smoother the gradient, but the higher the demands on paper and machine stability; the typical range is 150–200 lpi, confirmed with the printer and paper conditions.
- Large-area flat tints: large flat tints built from four-color overprint and long gradients are more prone to banding; changing to a spot color or a partial gradient noticeably lowers the risk.
- Total ink coverage: the limit follows the spec provided by the printer, with a common experience range of 240%–320%; exceeding it easily causes scumming and slow drying.
- Paper and equipment: paper with strong ink absorption swallows part of the fine color steps, while fluctuations in equipment condition can make the same batch inconsistent front to back.
The same gradient judged under a different output method should be judged by different standards. Below is a comparison of typical ranges; the proof result remains the final reference:
- Offset printing: stable color and suited to volume, but picky about large-area gradients — any instability in screening, ink/water balance, or paper will show. Better suited to materials that cannot compromise, such as brand colors and large-area base tints.
- Digital printing: flexible for short runs and version changes, with medium tolerance for gradients; by experience it suits small-to-medium formats and gradients with a modest span. Long gradients on very large formats still break easily; proofing lead time is commonly 1–3 business days.
- Large-format inkjet and photo printing: large format and long viewing distance mean banding of the same degree is often not obvious at the actual viewing distance, so requirements can be relaxed accordingly.
- Screen and online materials: no halftone dots or ink involved, so banding risk mainly comes from display devices and compression — a different logic from prepress, and not something to judge by print standards.
In other words, the common practice in 2026 is no longer to rework at the first sight of banding, but to first confirm who will see this material, at what distance, and under what lighting.
5. Where it applies and where it does not
Scenarios worth being strict about banding: large-area brand-color gradients, printed materials viewed up close (brochure covers, packaging, cards), banding that lands right in the visual center, and materials with a large print run. If problems occur in these cases, rework costs are high and the loss in brand impression is direct.
Scenarios that do not need over-processing: gradients that occupy only a small part of the image, large-format inkjet viewed from several meters or more, posters shown purely online, and rush jobs where neither budget nor schedule allows proofing. The basis for judgment is not whether banding exists, but whether it can be seen under actual viewing conditions and whether it affects the job this material is meant to do.
- A usable rule of thumb: take the proof to the actual viewing distance and look at it — if you cannot see it, there is no need to keep processing; if the stripes are visible at a glance, go back to the file side and narrow the span first.
- Not recommended: blindly deepening colors or increasing ink amount to suppress banding often trades one problem — banding — for another: large-area unevenness.
Frequently asked questions
Will adding noise to a gradient make it look dirty?
Light noise (experience range 1%–3%) is essentially invisible on printed materials; its role is to break up color-step jumps. Viewed close-up on screen it will show grain, so decide based on the actual use.
If a gradient looks smooth on screen, will it definitely band when printed?
Not necessarily. A screen is an emissive display with dithering, while printing relies on ink dots reflecting light; smooth on screen does not mean smooth in print. But for gradients with a small span and small area, most differences fall within an acceptable range.
Does it make a difference whether banding appears across the whole run or only on some sheets?
Yes, it does. Banding that is fixed in the same position across the whole run points more to the file or plate-making stage; banding that comes and goes and drifts in position more likely comes from ink/water balance, paper, or equipment fluctuations — and the path to fix it is different.
If text sits on top of the gradient, does that make problems more likely?
It does. Reversed-out or fine text on a gradient is already hard to control; it is recommended to switch the text area to a solid-color base, increase the type size appropriately, and verify against a physical proof before delivery.
For large-format inkjet gradients, do you still need to be that strict about banding?
It depends on viewing distance. On large images viewed from far away, banding visibility drops noticeably, so requirements can be relaxed based on actual distance; materials viewed up close are still best handled by print standards.
If you have a gradient version about to be released for print, check it in this order: first look at the gradient span and color mode, then ask the printer for a digital proof or a press proof, and finally decide based on actual viewing distance whether to add noise or adjust the screening. When the gradient area is very small and the viewing distance is far, there is no need to repeatedly rework for banding; large-area brand base tints and close-viewing materials deserve strictness, as these two are more easily caught by the eye. In project delivery, Xiyue Company usually fixes this step into the checklist before print release, so problems are not discovered only when the job reaches the press.
-
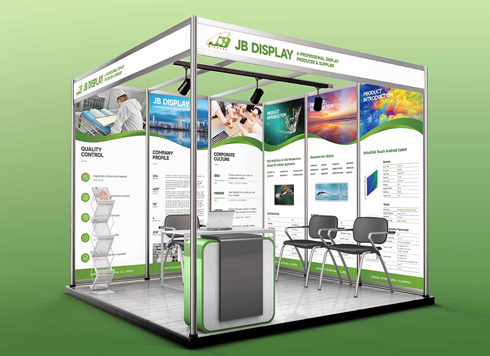 Booth Poster Design for Professional Monitor Product Suppliers
The standard exhibition booth poster projec ...
-
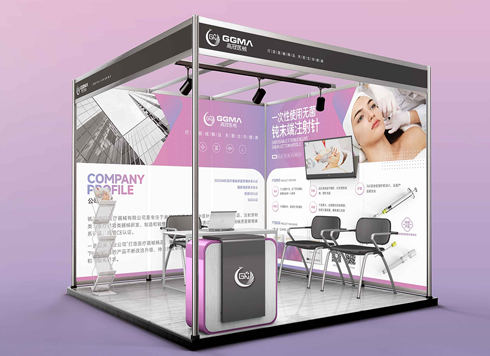 Design of Standard Exhibition Booth Posters for Beauty Instruments
Carefully designed a standard exhibition bo ...
-
 Design of Exhibition Posters for Medical Device Standards
XiYue is designing an exhibition booth post ...
-
 Collection of Brochure Design Cases in 2024 (Cover Series 02)
Our brochure design projects focus on diver ...
-
Why does the same foil stamping look premium on someone else's brochure but cheap on mine?
Date: Sep 14, 2026 Read: 1
-
Printed Black Text Looks Fuzzy with Color Fringing—Is Four-Color Black Really to Blame? Is It Necessary to Change Text Black Separately Before Printing?
Date: Sep 12, 2026 Read: 9
-
Will a QR Code on Print Really Fail If It's Printed Too Small? Do You Need to Test Scan with a Phone Before Output?
Date: Sep 11, 2026 Read: 11
-
Is 7pt Text on Printed Materials Really Unreadable? Is a Full-Size Proof Before Printing Necessary?
Date: Sep 10, 2026 Read: 15
-
How many fonts should you really use in a graphic design? Is more than three the actual deal breaker?
Date: Sep 9, 2026 Read: 18