Both the pen-barrel printer and the uniform embroidery vendor sent the logo file back—should versions have been separated from the start?
Conclusion first: whether to make a separate logo version for small items depends not on how large the item itself is, but on three things combined: how fine the thinnest strokes and negative spaces in the logo are, how fine a line the target process can hold, and how close people stand when viewing it. Based on common 2026 project delivery practice, for offset printing such as business cards and labels, the standard version is often enough; for pen-barrel screen printing or pad printing, fabric embroidery, and small on-screen icons, a simplified or one-color version is usually needed. Writing the size floor as “material + process + version + width range” is more actionable than giving a universal millimeter number.
Why the same logo file is not enough when moved to small items
Business cards are offset-printed, with a flat paper surface and a close viewing distance, so a logo can still keep its silhouette when reduced to a dozen or so millimeters. When moved to pen-barrel screen printing, fabric embroidery, or a 32 px icon, what changes is the output method: screen and pad printing have ink spread, embroidery builds shapes with stitches, and screens are constrained by the pixel grid. What people call blurriness is often not insufficient file resolution, but that the finer strokes and counters in the logo are already finer than the legibility floor of that process; proportional scaling does not automatically compensate.
- Fine strokes: screen printing, flexo, and embroidery each have a process floor for line width; below it, lines tend to break up or get thickened by ink.
- Negative space and counters: letter counters and graphic cutouts can easily be filled by ink or stitches at small sizes, appearing as a black blob.
- Processes cannot be converted into each other: the same millimeter number has no universal formula across offset printing, screen printing, embroidery, and screen pixels.
- Finishing changes edges: foil stamping, embossing, and lamination all affect edge clarity, more noticeably at small sizes.
So the usual judgment order is: first measure the logo's own details, then check the target process's typical range, then verify with a 1:1 proof or on-device preview—not set a number first and force everything into it.
Experience ranges for each material, and cost comparison of three approaches
Below are the more common value ranges in 2026 projects. Note that these are ranges, not standards; the specific values still depend on the printer's process sheet, proof, and actual print surface; the more detail a logo has, the closer to the upper limit, and bold geometric shapes can be closer to the lower limit.
- Business cards and letterhead, offset printing: overall width commonly 10–18 mm; horizontal versions with more detail should use the larger end.
- Packaging labels, offset or flexo: overall width commonly 12–20 mm; secondary graphics on small labels should be simplified.
- Pen barrels, screen printing or pad printing: one-color simplified version overall width commonly 8–15 mm; keeping fine lines at or above 0.15–0.25 mm is more stable.
- Fabric embroidery: overall width commonly 20–35 mm; fine lines are often thickened or merged, and counters need to be enlarged.
- Screen icons: 16–32 px usually requires simplified graphics; 48 px and above can use a more complete version.
- Outdoor large-format printing: viewing distance is far, overall width can reach tens of centimeters or more, and details scale up with distance.
The real decision is a three-way choice: scale down directly, make a separate simplified version, or only add a one-color version. None is inherently more professional; they fit different conditions.
- Directly scale down the standard version: extra design fee is usually 0, turnaround about 0–1 working day; suitable for distant-view large-format printing and large on-screen graphics; the trade-off is that details may blur on small items.
- Make a separate small-size simplified version: typical cost experience range is several hundred to two or three thousand RMB, turnaround about 2–5 working days, usually including 1–2 rounds of proofing; suitable for pen barrels, hang tags, embroidery, and icons.
- Only add a one-color or reverse-white version: typical cost experience range is several hundred to 1,500 RMB, turnaround about 1–3 working days; suitable for screen printing on dark backgrounds, but it does not solve structural detail issues.
When it is worth doing, and when it can wait
If the same logo needs to appear on business cards, packaging, pen barrels, embroidery, screen icons, and other media, and suppliers are dispersed with files resent each time, writing size floors into the guidelines is more valuable: it turns “I think it is legible” into proofable, acceptable criteria and reduces repeated rework on small-batch materials.
- Recommended: cross-material implementation, need for basic visual guidelines, promotional product screen printing, uniform embroidery, multi-vendor handoff.
- Can wait: only used for large-format graphics viewed from a distance; the logo itself is just two or three bold strokes with no fine lines or complex negative space; budget is very tight and only one-off large-size materials are needed.
- Do not confuse: screen-pixel floors cannot be directly converted into print millimeters, and print floors cannot be directly applied to embroidery.
A delivery-site experience: the proofing step cannot be skipped
In one project, the constraints were only 5 working days, a tight budget, and the client would provide only one color horizontal logo version, yet it had to be applied simultaneously to 3,000 gel pens by screen printing, 200 uniforms by embroidery, and a batch of hang tags. The approach was to first make 1:1 proofs at target sizes, with one set each for the pen barrel and embroidery: the small line of text in the horizontal version blurred into a blob on the pen barrel, and the counters were also filled by stitches in the embroidery proof. So it was changed to a simplified version of “graphic mark + fine lines thickened to about 0.2 mm,” and the embroidery version was enlarged by one more step.
As a result, the schedule was delayed by about two days, with extra proofing and revision costs, in the experience range of several hundred RMB. The cost was real, but compared with reworking the whole batch of 3,000 pens plus 200 uniforms, it was worth it. In typical ranges, the closer a size is to the process floor, the more margin should be left; do not finalize at the critical value where it is just barely recognizable.
Acceptance: look at details, not just the outer contour
At acceptance, first check the 1:1 proof or on-device preview at the target size, then check whether fine strokes are continuous, whether negative spaces are blocked, and whether the outer contour is still recognizable, and finally verify whether different materials are separately marked with size and process notes. In typical ranges, failures often occur not in the outer contour but in counters and fine lines.
- Acceptance criterion: on the target material and at actual size, the brand name or graphic features are recognizable without leaning in.
- Acceptance criterion: delivery includes vector standard, simplified, and one-color or reverse-white versions, with their applicable ranges marked.
- Failure signal: only a generic width number is provided, or an enlarged on-screen preview is used instead of a physical proof.
FAQ
Is a 10 mm wide logo enough on a business card?
A 10 mm width can work on a typical offset-printed business card if strokes are relatively bold and negative space is large enough; for horizontal versions with more detail, a more stable typical range is 12–18 mm. Confirm with a proof at actual size.
For a logo screen-printed on a pen barrel, how much should fine lines be thickened?
There is no uniform thickening amount. The experience range is to keep fine lines at or above 0.15–0.25 mm while enlarging counters and stroke spacing; the specific value depends on the pad-printing or screen-printing process sheet and a 1:1 proof.
Why does a logo for uniform embroidery need to be larger than the print version?
Embroidery builds shapes with stitches, and fine lines and narrow negative spaces are easily filled by stitches. Overall width commonly needs to be 20–35 mm, fine lines are often thickened or merged, and counters need more space.
Can a 32 px on-screen icon use the standard version directly?
At 16–32 px, it is usually not recommended to use the standard version directly; simplify the graphic or remove secondary text. At 48 px and above, a more complete version can be used, and the safe area should be checked against each platform's icon guidelines.
If we already have a vector file, why does it still blur at small sizes?
Vector only ensures no pixelation when enlarged; it does not ensure details remain legible at small sizes. Fine strokes, negative space, and the printing process still limit the floor. In such cases, a simplified or one-color version is usually needed.
Action guide: first list the materials and processes where the logo will be applied, then make 1:1 proofs at target sizes, and write the applicable ranges of the standard, simplified, and one-color versions into the delivery guidelines. This approach applies to cross-material, multi-vendor, or small-size materials; if only distant-view large graphics are needed and the logo itself is very simple, there is no need to add a separate revision round for this.
-
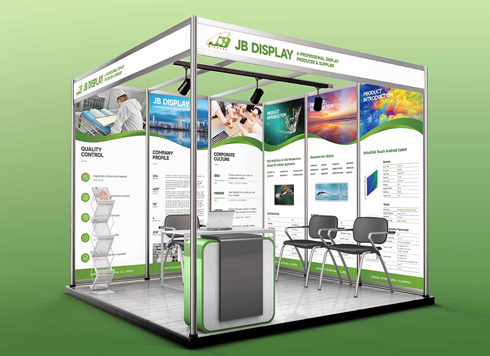 Booth Poster Design for Professional Monitor Product Suppliers
The standard exhibition booth poster projec ...
-
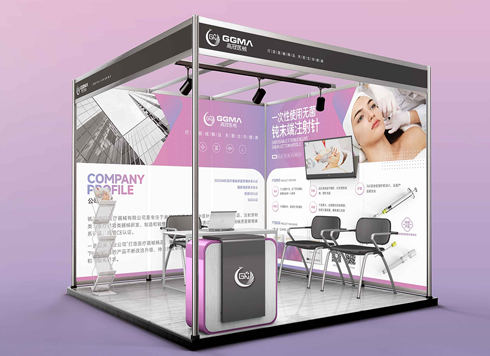 Design of Standard Exhibition Booth Posters for Beauty Instruments
Carefully designed a standard exhibition bo ...
-
 Design of Exhibition Posters for Medical Device Standards
XiYue is designing an exhibition booth post ...
-
 Collection of Brochure Design Cases in 2024 (Cover Series 02)
Our brochure design projects focus on diver ...
-
When an A4 one-pager is scaled straight to A5 for print, where does it feel cramped first if font sizes and margins are not rechecked in millimeters before printing?
Date: Oct 19, 2026 Read: 11
-
Where does a semi-transparent white overlay on a cover photo fail first if it is not flattened before printing?
Date: Oct 18, 2026 Read: 12
-
Brochure spread photo has a strip eaten away in the middle—what number should you ask the printer before going to press?
Date: Oct 17, 2026 Read: 13
-
For a packaging box with a round window, should the window position be set by the designer in the artwork first, or wait until the printer's die line is ready?
Date: Oct 16, 2026 Read: 17
-
The logo is centered in the circular button, so why does it still look off to one side? Should I nudge it manually, or is something wrong with the file?
Date: Oct 15, 2026 Read: 16